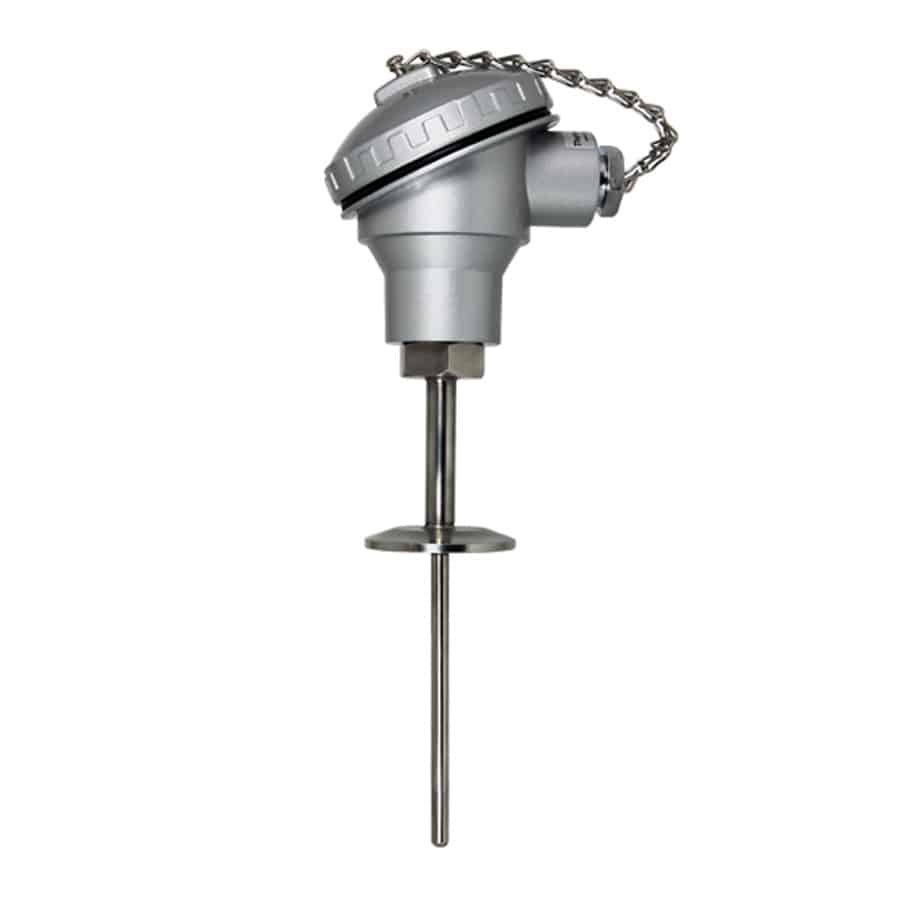
Improve pump protection and process reliability with our PT100 temperature sensors.
Designed to monitor temperature increases within metallic pump systems, these resistance temperature detectors provide accurate measurement of process conditions and early warning of potential operating issues before they develop into costly failures. The sensor measures temperature directly from the isolation shell area.
A rise in liquid temperature can indicate problems such as closed-valve operation, reduced flow conditions or abnormal pump operation, across a wide range of chemical and industrial applications.